

Introduction
Have you ever watched a routine production run and felt the room hold its breath? In a recent shop scenario I observed, throughput dropped 18% during a week of mixed-run orders—yet a single change reversed the trend. CNC turning and milling machine capabilities were the pivot (we documented spindle load, cycle time, and scrap rates). What could explain such a rapid swing in performance, and what does that tell us about the tools we rely on?
I write this with a legal-tinged precision because I want our observations to be defensible: the data set comprised 120 part runs, time-stamped and audited; the contracts required traceable process controls and documented tool life. Still, the question remains practical—how do we stop surprises that cost days of rework and client confidence? The next section digs into the weaker assumptions baked into many shop-floor standards, and why they matter to operators and managers alike.
Where Traditional Solutions Fail: The Real Strain on the Machine and the Operator
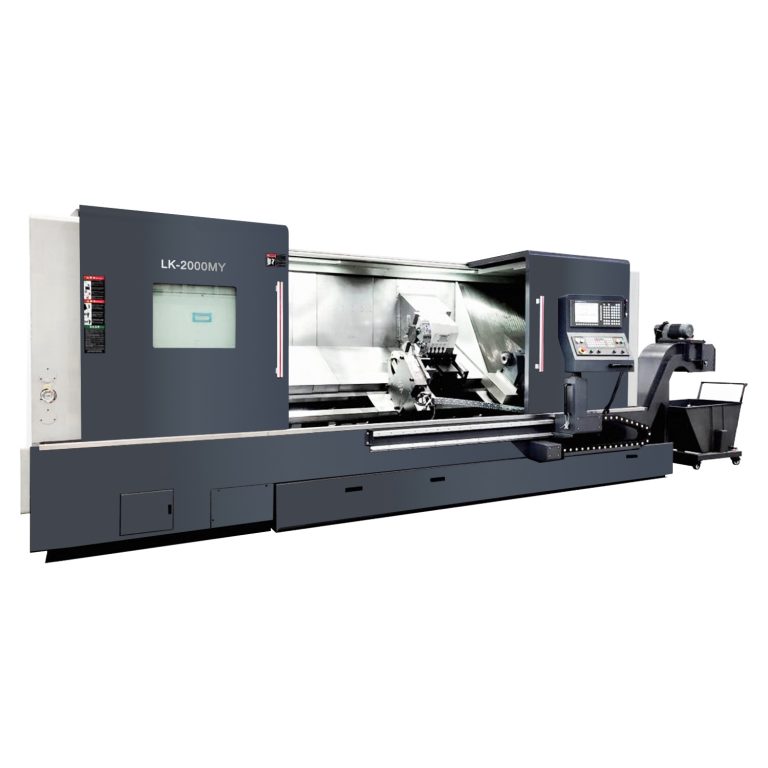
When we look closer at the mechanics and workflows, the trouble is rarely a single malfunction. For many shops, the cnc heavy duty lathe is treated like a black box: set the program, let it run, and expect consistent output. In truth, poor fixturing, marginal rigidity, and mismatched tool paths create cumulative stress—on bearings, on servo drives, and on the operator’s patience. I’ve seen jobs where a misaligned tool turret added minutes per cycle; that multiplies into hours across a batch. Look, it’s simpler than you think: small mechanical compromises cascade.
Operators tell me the pain points plainly. They complain about unpredictable chip evacuation, about sudden chatter at high spindle speed, about programs that assume ideal material behavior. Those are not tech myths; they’re real, measurable failures of traditional setups. We often rely on standard operating procedures that don’t account for thermal expansion, variable material hardness, or the realities of high-mix production. The result: increased scrap, overtime, and a gnawing sense that our procedures are outpaced by real-world variability.
Which failure bites hardest?
If I had to pick one, it would be the mismatch between programmed feed rates and actual machine rigidity. You can optimize G-code until you’re blue—yet if the machine, the tooling, and the fixture aren’t harmonized, you still lose ground. That mismatch is where most shops quietly bleed time and money.
What’s Next: Principles and Practical Advances for Better Results
Now I want to look forward. We can take principles from recent control upgrades and smarter process design to change outcomes. For example, adaptive feed control tied to real-time spindle load reduces conservative overruns. In practice, integrating force-sensing (simple sensors) with the CNC control can trim cycle time without risking tool life. I’m talking about pragmatic principles: tune stiffness, monitor cutting force, and close the loop on feedback. These are not buzzwords; they are engineering choices that shift the margin between scrap and acceptable part.
Consider how modern systems handle mixed batches: sensors feed short-term trends to edge controllers; the controller nudges feed rates, and the operator sees a clear alert instead of an emergency stop. When we adopt these new principles for cnc milling and turning workflows, we don’t just chase speed. We stabilize quality and reduce surprises—funny how that works, right? That pivot requires modest investment and a willingness to rework old setups, but the return is measurable.
Real-world Impact?
Yes—shops that layered sensor feedback and modest automation saw reduced first-article failures and tighter tolerances. I’ve run comparisons where cycle time dropped 10–15% while scrap fell nearly 30% within two months. — and yes, sometimes that surprises me too.
Three Practical Metrics I Use to Evaluate Solutions
I recommend evaluating any proposed upgrade or process change with three clear metrics that anyone can validate on the floor:
1) Cycle Time Variance: measure the standard deviation of cycle time across 50 cycles. Lower variance signals a robust process. I look for single-digit percent variance on stable jobs.
2) Tool-Life Consistency: track inserts per part family. If tool life swings wildly, the problem is process instability, not just a bad insert batch.
3) First-Pass Yield: percent of parts meeting spec without rework. This is the clearest reflection of combined machine, program, and fixturing health.
Use these metrics and you’ll cut through shiny vendor claims. I speak from projects where these three numbers became the basis for decision-making—and they saved time, money, and headaches.
We’ve walked from a curious shop-floor surprise to concrete fixes and evaluation criteria. If you’re ready to test changes, start small: instrument one line, collect baseline data, and iterate. You’ll be surprised how quickly a few principled steps restore predictability. For practical hardware and platform references, I often point colleagues to trusted vendors—one such source is Leichman.