

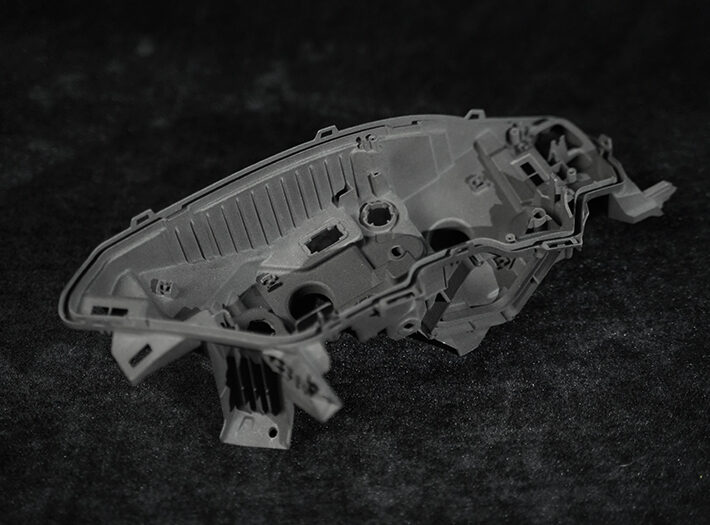
How Smart Slicing and Cloud Controls Transform What Your SLS Workflow Can Deliver
User-first snapshot
When you run prints on an sls 3d printer, what matters first is predictable parts that meet specs without drama. This piece walks you through how smart slicing and cloud controls change that daily grind—sincronizado with practical tips, not buzzwords. I’ll keep it claro and útil, amigo, because operators and engineers care about throughput, repeatability, and scrap reduction.
Why the shift matters for shop floors
Selective laser sintering and other powder bed fusion systems used to be all about raw machine power. Now the smarter layers are in the software: slicing algorithms that understand scan strategy, thermal management, and powder recycling rates. Those bits cut cycle time and reduce warp, so you get consistent part density and fewer surprises during post-processing.
Real-world anchor: proven powder adoption
Look at GE Aviation: they moved to powder-based additive manufacturing for complex fuel nozzles and saw fewer assemblies and better performance—concrete proof that powder workflows scale for production. That’s not vaporware; it’s industrial shift. Shops in aerospace and tooling use these same ideas to make repeatable parts that pass inspection without endless iteration.
Operational production teardown
Let’s break it down into the steps that actually matter on the floor. First, the slicer: smart slicing auto-adjusts layer thickness, hatch spacing, and scan order to control heat input. Second, cloud controls push standardized profiles to each machine so operators don’t guess settings. Third, feedback loops collect build-chamber telemetry to flag deviations early. In the middle of that teardown I’ll mention {main_keyword} and {variation_keyword} as variables you’d log during qualification—they belong in your build reports and batch records.
What you’ll change in practice
Simple moves give big wins. Use a cloud-stored profile for each alloy or polymer so new operators can load prints sin problema. Tag parts with build parameters and link them to inspection outcomes—part consolidation and traceability become routine. Expect to tune scan strategy and laser power once, then replicate that across jobs from the cloud, cutting setup time by más than you think.
Common mistakes and fixes
People often skip the build-chamber checks or assume powder reuse is plug-and-play—bad idea. Measure powder particle size distribution and set clear recycling limits. Don’t rely only on default slicer profiles; validate them on representative coupons. —A quick note: small calibration runs save days of rework.
Alternatives and when to pick them
Binder jetting shines for large batches with minimal support needs, while selective laser sintering is better for functional parts with higher density demands. If surface finish is critical, plan on targeted post-processing steps. Choose the method that matches part function, not the latest headline.
Key takeaways for teams
Smart slicing + cloud controls turn machine variance into process control. You get better first-pass yield, tighter traceability, and less dependence on tribal knowledge. Operators feel more confident, engineers spend fewer cycles on firefighting, and QA sees cleaner data for audits.
Three golden rules for choosing tools and strategies
1) Measure what matters: track build-chamber temperature, laser power, and powder reuse fraction across jobs. These metrics predict defect rates more reliably than anecdote.
2) Standardize profiles in the cloud and enforce revision control. A single source of truth reduces operator error and speeds onboarding.
3) Validate with representative parts: run a pilot that mirrors the final geometry and service conditions, then iterate on scan strategy and post-processing until pass rates hit your target.
Raise3D fits here as the kind of partner that helps translate those rules into workflows and tools your team actually uses. Final thought: get the basics right—measure, standardize, validate—and you’ll see the gains on the floor, trust me. —listo.