

Introduction — A Question That Sticks
Have we mistaken complexity for excellence in our shops? I ask that because I’ve stood on the shop floor and watched a promising line of work stall for lack of simple alignment — not strategy. As a consultant who speaks regularly with vertical machining center manufacturers, I see patterns in downtime, quoting, and delivery times that the figures make plain: industry reports show cycle-time variance up to 18% between similar machines (and that’s no small sum). What’s driving those gaps?
We now measure spindle speed, tool changer reliability, and servo motors’ response as routine KPIs, yet something less tangible often decides success — service cadence, staff training, spare-parts logistics. I’m compelled by data and by faces; there’s a human strain behind every missed deadline. In Edinburgh I’d say we must be blunt about it — solutions are rarely only hardware. So let’s unpack what’s really at fault next, and see where practical fixes might sit.
(Aye, I’ll be direct: this piece will call out flaws and point to real choices.)
Next, I’ll examine the parts that crumble first — and why those failures keep recurring.
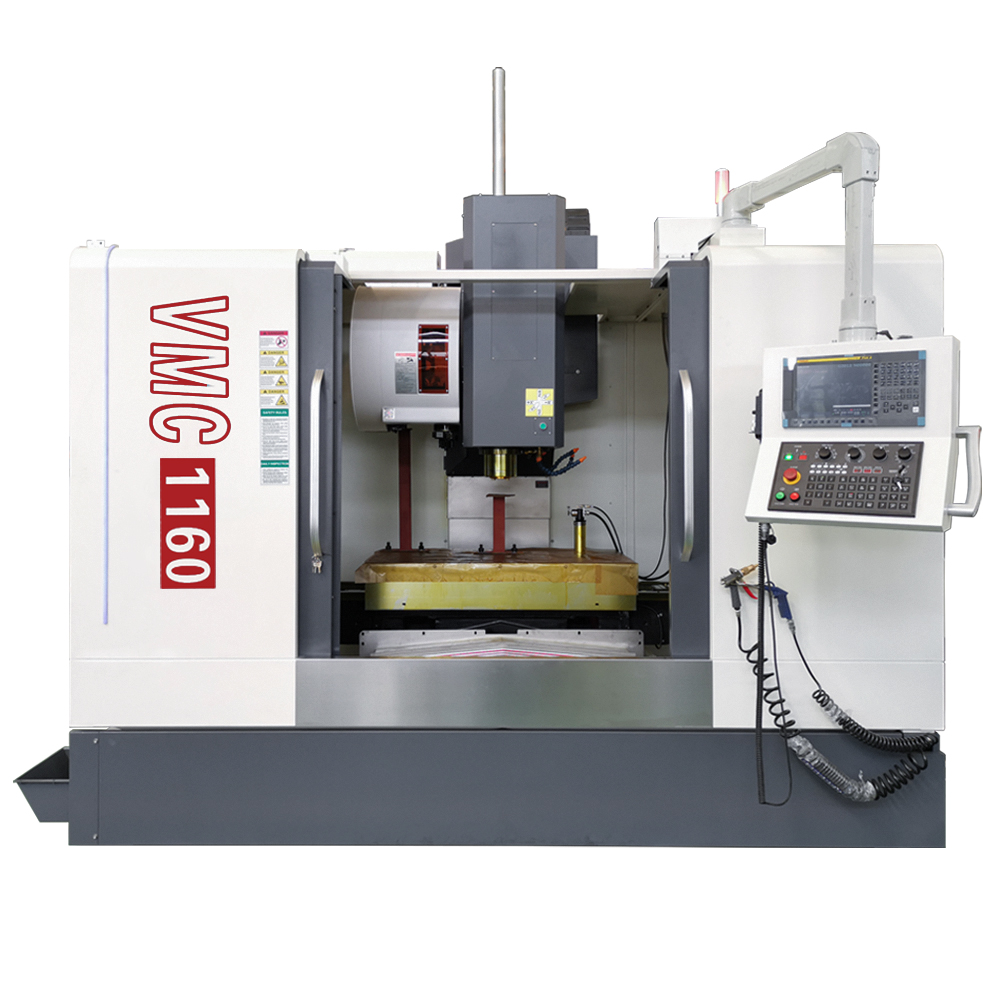
Technical Drill-Down: Hidden Flaws and User Pain Points
When I test a horizontal or vertical turning machining center, I begin with the control loop and then watch users. That order matters: the CNC controller’s settings and the ball screw backlash show up faster in the shop than any glossy spec sheet. In plain terms, many systems look great on paper — spindle speed, tool changer cycles, and coolant system ratings — but their real-world resilience is weaker. I see two recurring failures: misaligned maintenance plans and overloaded operators who never got time to learn the HMI. Look, it’s simpler than you think: a poorly tuned servo system will cost you hours per week; a confused operator will cost you days.
What breaks first?
First, routine maintenance gets deferred. Bearings and power converters age quietly; you don’t notice until chatter rises or the axis lags. Second, software defaults are rarely tuned to the workshop’s material mix — aluminium one week, hardened steel the next — so tool life and cycle times swing wildly. I’ve felt the frustration in engineers’ voices; they’re pragmatic, often angry, and rightly so. — funny how that works, right? The result? Higher reject rates, longer setups, and a creeping need for expensive retrofits. These are operational pains, not marketing problems.
Forward-Looking Principles: New Tech and Practical Metrics
What we need next are principles that guide real choices. I’m talking about pragmatic adoption: better diagnostics, modular upgrades, and clearer downtime analytics. Take the rise of embedded edge analytics that sit beside the CNC controller — they report spindle speed variance, torque spikes, and tool-wear trends in near real-time. When paired with predictive maintenance routines, that data prevents unplanned stops. If you evaluate a 5 axis vertical machining center today, ask how its architecture supports diagnostics, not just top-end specs. I’m keen on systems that let you swap a module without a week-long halt; serviceability matters almost as much as peak throughput. — and yes, that changes ROI math.
What’s Next for Manufacturers?
We should favour machines designed for incremental improvement: open interfaces for condition monitoring, standardized tool-changer modules, and accessible training materials baked into the HMI. These lessen dependence on specialist technicians and give shop-floor teams ownership of uptime. To choose wisely, I recommend three clear metrics: mean time between failure (MTBF) under your material set, mean time to repair (MTTR) with available parts, and net cycle-time consistency over 30 days. Measure these, compare suppliers, and you’ll stop buying promises; you’ll start buying predictable output.
In my work I’ve seen suppliers who promise “fully integrated” platforms but deliver systems that fracture under mixed production. We must judge by measurable recoveries and not by brochure blurbs. If you want a partner who understands those trade-offs, have a look at Leichman — they build with serviceability in mind and they know the cost of a stalled line.