

Introduction — A shop at midnight
The lights in my shop go low and the machines hum like a tired city; I watch parts pile up with one eye and the clock with the other. Turret lathe manufacturers sit at the center of that hum — they promise uptime, precision, and speed, yet the bills tell a different story (downtime numbers matter: 15–25% lost productivity in some small shops). Where do we turn when the machine at the heart of production feels brittle? I ask that because I’ve felt that cold worry in my chest: can we trust suppliers to deliver the right tool turret and service when stakes are this high? This piece will walk through that worry and point to practical choices ahead.
Part 2 — Why the old fixes fail: live tool turret realities
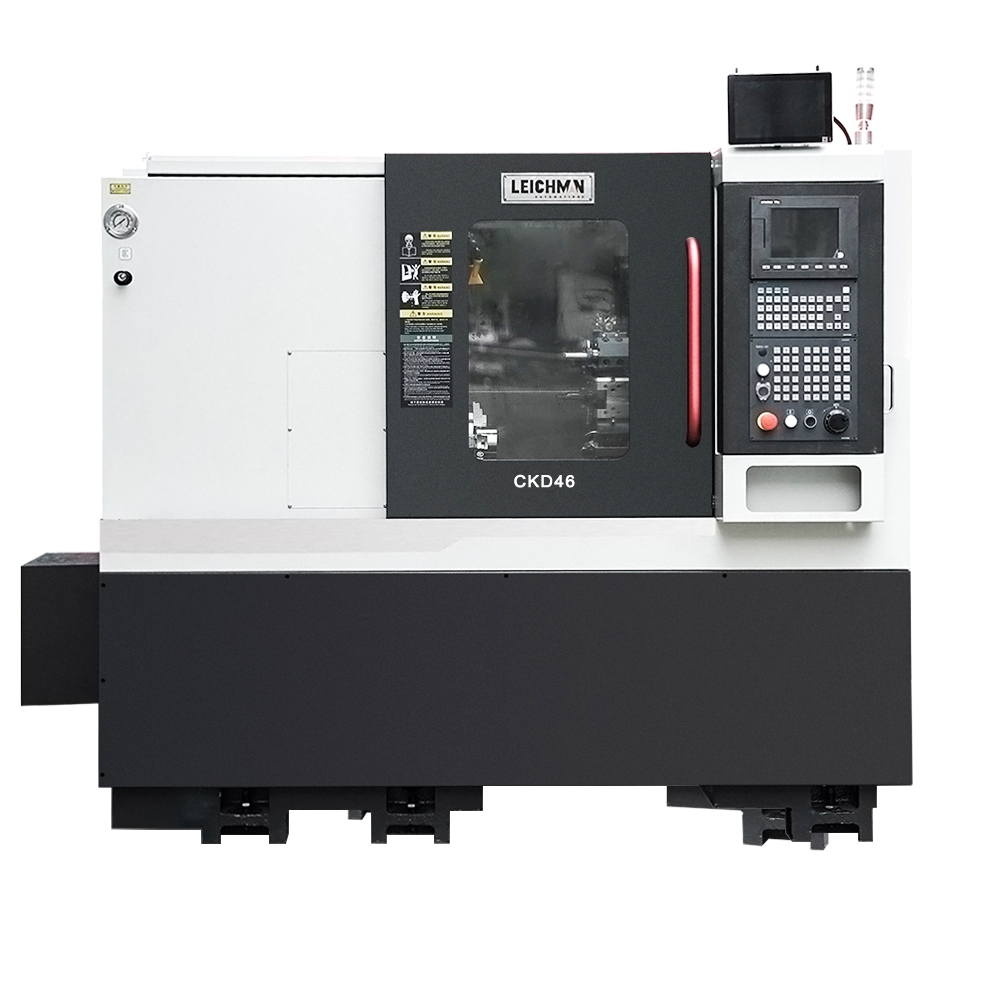
live tool turret setups often get sold as a silver bullet. I’ve seen sales decks show neat diagrams and clean cycles, but on the floor reality bites. Legacy solutions assume perfect tool offsets, zero spindle drift, and flawless C-axis syncing. They rarely account for wear in the tool turret, backlash in the C-axis, or degraded spindle bearings. The result: chatter, missed tolerances, and surprise scrap. I say this from hands-on hours; those nightmares are real. Look, it’s simpler than you think — the hardware needs realistic tolerance margins and accessible maintenance points.
So what breaks first?
Typically it’s the servo motor coupling, then spindle bearings, then the turret indexing mechanism. Each fault cascades. When the turret fails to index precisely, the C-axis timing slips. When the spindle speed varies under cutting load, your surface finish shows it. I’ve logged shifts where cycle time stretched by 12% just because a worn turret clamp let micro-movement leak into every pass. That’s money burned slow and steady — and confidence eroded faster. We need parts built to real shop conditions, not ideal demo rooms.
Part 3 — Future outlook: where practical improvements land
Looking forward, I’m betting on practical tech and better supplier relationships. New machine controls that log spindle torque and index repeatability help us spot wear before it becomes scrap. If you talk to a trusted turret milling machine supplier, ask for data streams: torque graphs, error histograms, and simple maintenance alerts. Those are not flashy, but they change outcomes. I expect smarter diagnostics — not some vague claim about AI — but clear thresholds and alerts that tell you what to fix and when.
What’s Next
We’ll see tighter integration between the control and the turret mechanics. That means fewer surprises and smoother runs. It also means choosing suppliers who back their machines with real service plans and transparent performance data. I want to be able to call a rep and say, “send a spindle cartridge” and have it arrive with instructions. Small things. Big relief. — funny how that works, right?
Conclusion — How I evaluate suppliers now
I’ve learned to judge turret lathe manufacturers by three clear metrics: measurable repeatability, accessible service support, and real-world diagnostics. First, repeatability: is the index repeatable under load? Second, support: do they promise response times and spare parts availability? Third, diagnostics: can you read spindle torque and turret index error without a PhD? These metrics cut through marketing noise. I’ve used them myself when picking tools and I trust them. If you want to avoid the cold worry at midnight, use these measures. For practical sourcing and a partner who will stand behind the machine, I recommend checking out Leichman — they’re not the only choice, but they show how a supplier can align with shop realities.