

Introduction: A Shop-Floor Moment, Some Numbers, and a Simple Question
I remember walking into a small job shop where the lead machinist sighed over a stalled run — and that little pause told me everything. When teams hunt for cnc equipment for sale, they often expect plug-and-play solutions but get downtime instead. CNC equipment manufacturers are juggling feature lists, warranty claims, and support tickets while shops track OEE and lead times (and yes, morale dips too). Data shows mid-size shops report machine downtime eating 8–12% of scheduled production — so how do we turn that around without breaking the bank? I’ll walk through the real pains and the fixes that actually stick. Next, we’ll peel back what typical “quick fixes” miss and why operators keep calling for help.
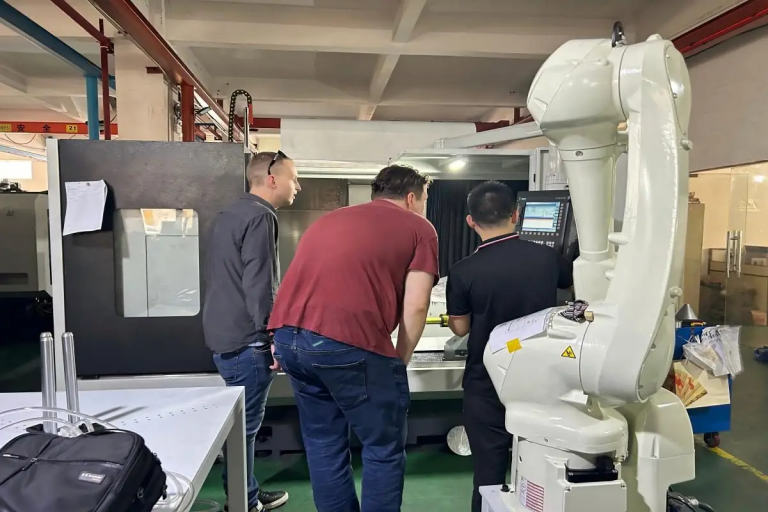
Where Most Fixes Fall Short — The Hidden Pain Points
Look, a lot of solutions are sold as silver bullets, but they’re not. Many shops get a diagnostic checklist and a spare part, then call it a day. That misses the human side — operators know the machine’s quirks but can’t always convince purchasing to invest. Technical gaps matter too: older CNC controllers and servo motors can behave fine most of the time but fail under thermal drift or fluctuating supply (power converters get stressed). The result is intermittent errors that are hard to reproduce. I’ve seen shops replace a spindle drive only to find the root cause was a loose grounding strap feeding noise into the controller — funny how that works, right? — and the replacement never addressed the electrical noise, so the failure recurs.
What’s the real problem?
Often it’s a stack of small issues adding up: misaligned tool holders, outdated firmware, poor shop-floor network segmentation, or edge computing nodes that aren’t tuned for low-latency telemetry. These combine to make diagnosis take longer and parts look like the easy scapegoat. We need to stop treating symptoms and start mapping failure modes to daily workflows. I prefer short, frequent checks the team can run — not a 50-step audit no one finishes. That approach saves time and keeps the data meaningful.
Forward-Looking Fixes: Principles and Practical Picks
Moving forward, I lean on principles more than features. First, aim for predictable performance: monitor vibration, spindle temp, and current draw continuously. Second, standardize firmware and network configs so remote diagnostics actually work. Third, pick machines that give clear fault telemetry — that’s worth the premium. If you’re shopping, look at the whole ecosystem when you search for cnc machine for sale — not just spindle RPM or axis travel. Case in point: a small manufacturer I worked with swapped to machines with built-in condition monitoring; their unscheduled stops dropped by half in three months. It wasn’t magic — it was data plus better maintenance planning.
What’s Next — Real-world Impact?
Here are three quick metrics I use to evaluate options: 1) Mean Time To Detect (MTTD) — how fast does the system flag a degrading condition? 2) Diagnostic Clarity — can your team or remote support pinpoint the subsystem (drive, controller, spindle) within one go? 3) Support Turnaround — how soon do you get a meaningful update or firmware fix? Use these to compare vendors and models. I recommend running a 60–90 day trial on one critical cell before rolling out changes across the plant. It’s low risk and gives real operational insight — and I’m telling you, that will save both money and headaches.
To wrap up: we should prioritize practical diagnostics, simple operator checks, and clear telemetry. I’ve seen manufacturers succeed when they treat maintenance as part of the product, not an afterthought. If you want help building a short checklist or picking metrics, I’ll happily share templates. For trusted gear and vendor support, consider the offerings from Leichman.