

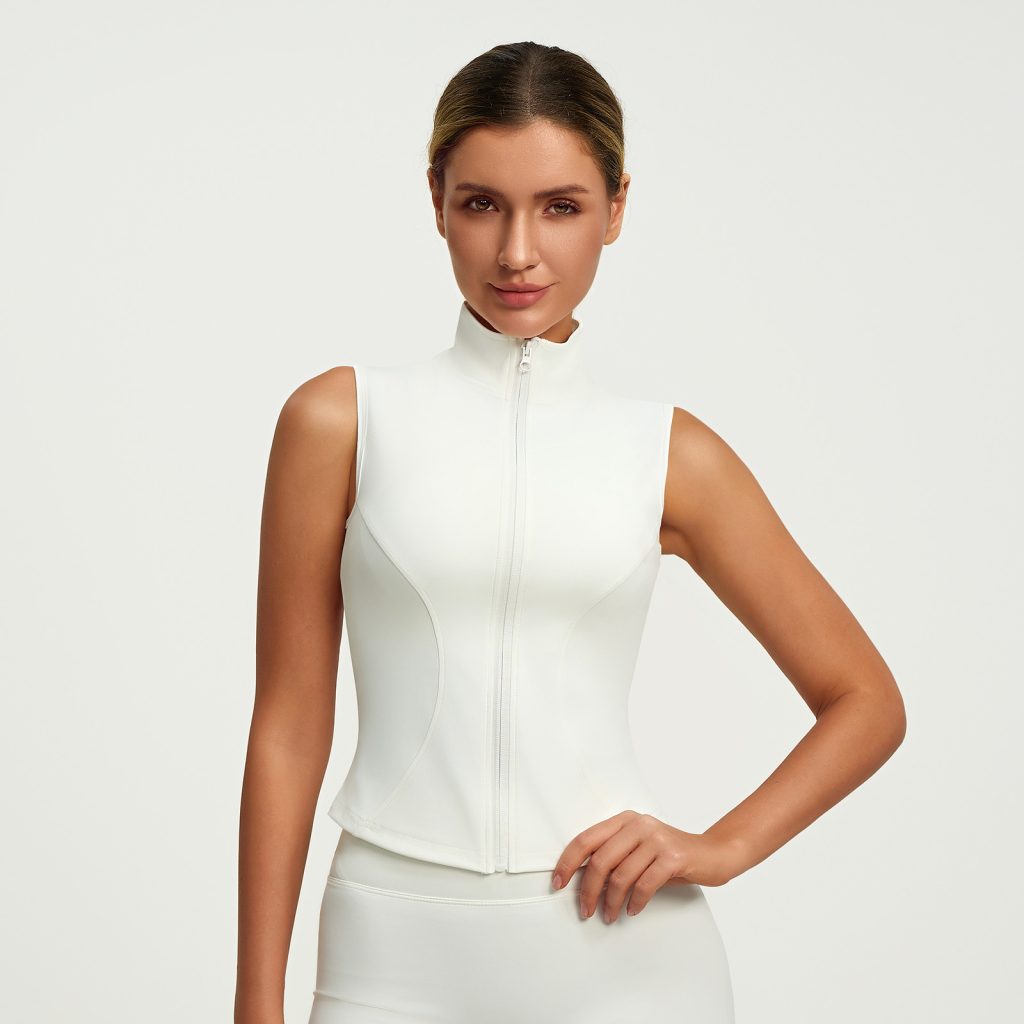
Setting the table: why a comparative lens matters
Think of wholesale production like a busy kitchen: you need mise en place, steady heat, and exact timing to deliver the dish consistently. Buyers in Los Angeles and other urban hubs expect repeatable fit and fabric performance after the 2020 retail shifts, so the choice of factory process changes margins and reputation. This piece compares batch-driven mills, cut-and-sew ateliers, and integrated lean lines to show where cost, speed, and quality meet—while noting how a focused supplier can also deliver complementary pieces like custom yoga jackets without compromising the pant run.
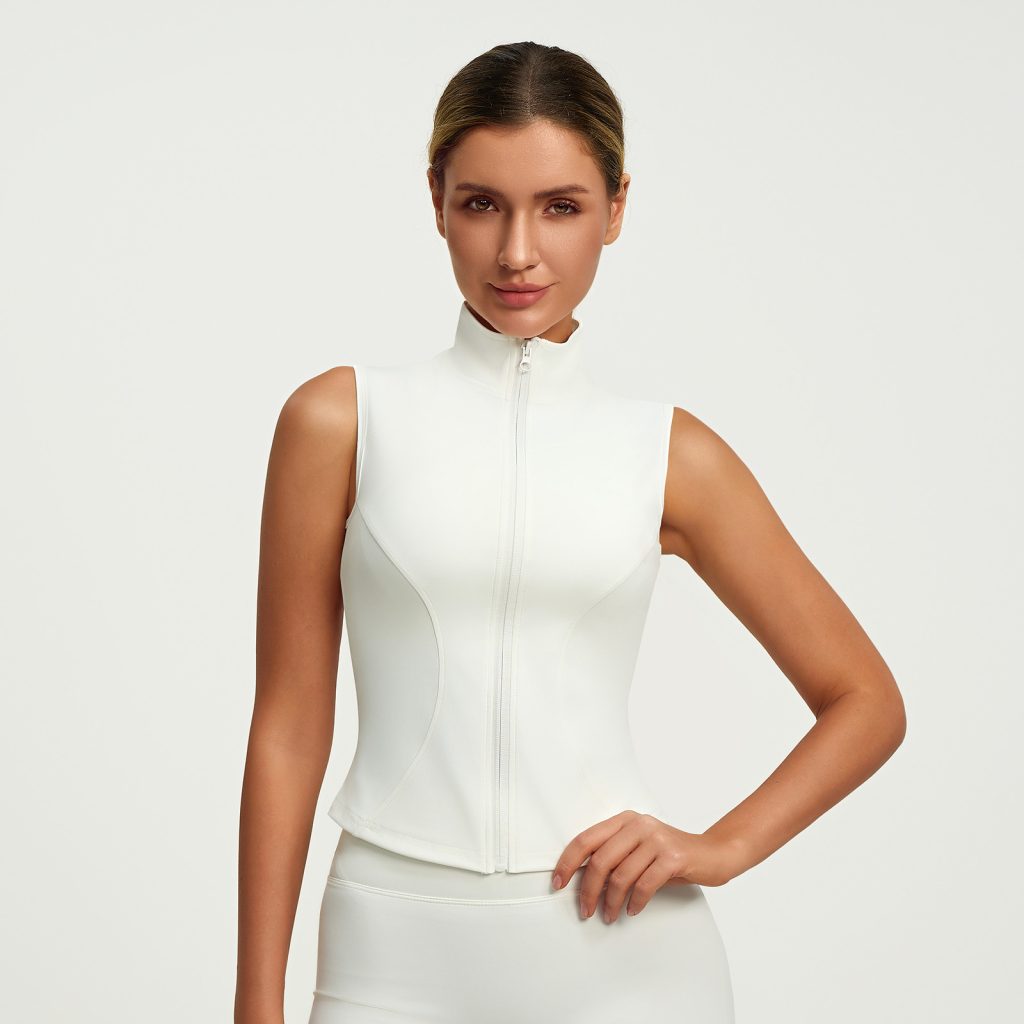
The taste test: factory methods compared
Batch-driven mills scale with tooling and offer lower unit cost for large runs, but they can flatten detail—think mass-steamed bread versus hand-shaped rolls. Cut-and-sew ateliers excel at small-batch nuance: pattern grading, flatlock seams, and precise waistband engineering. Integrated lean lines bridge both: four-way stretch materials and automated cutting give speed, while manual finishing preserves hand-feel. For women’s yoga jackets, the same comparisons hold: bonded hems and anti-odor treatment may be automated, but hood shaping often benefits from artisan finish.
Operational production teardown
Start by mapping inputs like a recipe: material specs, trim list, grading rules, and lead time. Then pare the method down to yield and waste. In practice, the checklist reads like: fabric inspection -> marker planning -> automated cutting -> assembly -> QA pass. This is where {main_keyword} and {variation_keyword} belong—embedded into engineering docs so pattern makers and line managers operate from one source of truth. Four-way stretch and performance knit require tension controls on machines; compression fabric needs staged steaming to set shape. Keep records by run to trace defects back to exact lot numbers.
Material and finish: flavors that sell
Fabric choices are the spice rack. Moisture-wicking knits and anti-odor treatment are popular, but finish and hand determine reorder rates. Flatlock seams reduce chafe; bonded hems lift aesthetics but add process steps. A good supplier sources performance knit with stable dye lots and tests for pilling and shrinkage; those micro-decisions lower returns and increase lifetime value. Smaller brands often trade lower MOQ flexibility for more refined detailing—an exchange worth measuring.
Alternatives and common mistakes
Some buyers chase the cheapest per-piece price and discover late that factories skimp on seam allowances or skip pre-wash, leading to mismatched sizes after first wash. Others over-spec trim choices and bloat cost. A middle path mixes clear tech packs with approved samples and a measured pilot run—cook a small batch first to taste. —Don’t omit field-testing on instructors or studio staff; real wear reveals issues lab tests miss.
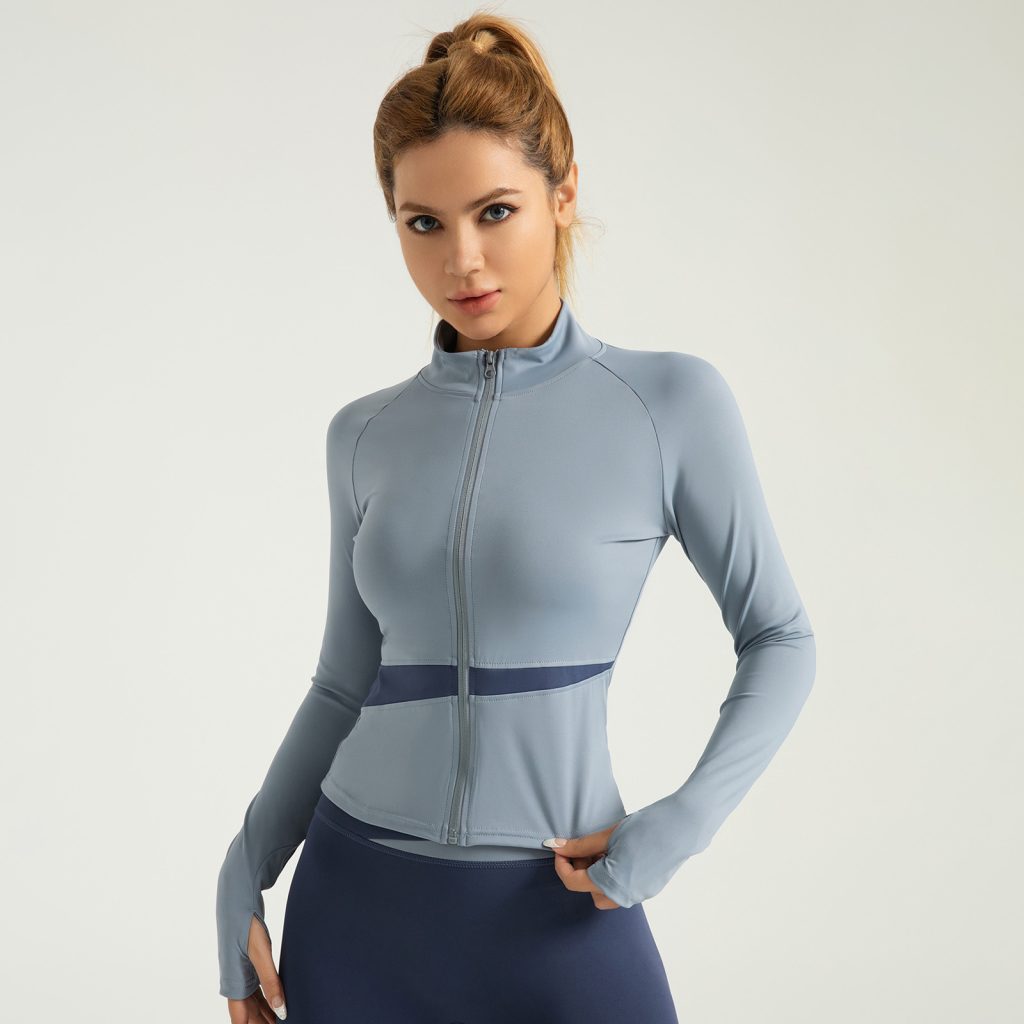
Comparative checklist for sourcing partners
Use this compact rubric when tasting factories:
– Fit repeatability: documented size ranges and pilot sample history.
– Fabric traceability: roll numbers, shrinkage rates, and dye-lot records.
– Process transparency: on-floor photos, stitching standards, and QA thresholds like seam tensile strength and wash cycles logged.
Advisory: three golden rules for choosing a partner
1) Prioritize reproducible samples over low quotes. A stable first run beats an uncertain bargain on reorder.
2) Demand material traceability and smallest acceptable variance numbers for four-way stretch and compression fabric—these are your quality anchors.
3) Insist on a short pilot run with clear acceptance metrics for fit, color fastness, and pilling. If a partner resists, they may be masking process gaps.
Measured sourcing decisions turn design intent into reliable product on the mat; the right balance of automation and hand work keeps margins healthy and customers coming back. Joebond. –